Global demand for lightweight, corrosion-resistant components is reshaping industrial sourcing. Aluminum Extrusion Parts now support frames, heat sinks, solar structures, machine guards, and transport systems. The applications look different, but buyers usually face the same questions: Can the supplier hold tight tolerances? Can it maintain quality across repeated batches? Can it ship reliably across borders?
Grand View Research identifies construction, transportation, and industrial applications as major growth drivers in the aluminum extrusion market. The International Aluminium Institute also reports sustained global demand for aluminum in lower-carbon manufacturing and infrastructure. These trends matter because extrusion performance depends on more than alloy selection. Die design, billet quality, surface treatment, cutting accuracy, packaging, and inspection records all influence the final result.
Small details matter.
A scratched anodized profile can delay assembly. A slight dimensional shift can increase machining costs. Poor export packaging can damage otherwise compliant parts. This guide evaluates seven suppliers for global buyers through practical criteria, including extrusion capacity, alloy availability, finishing options, quality systems, customization experience, lead times, and international logistics. Supplier information is considered alongside recognized industry standards and published capabilities, rather than marketing claims alone.
No supplier is perfect. A factory strong in high-volume construction profiles may not suit complex CNC components. A low quoted price may exclude tooling, testing, or protective packaging. Buyers should verify certifications, sample approval procedures, inspection methods, and commercial terms before placing significant orders. The following suppliers offer credible starting points, but careful technical review remains essential. geschniegelt
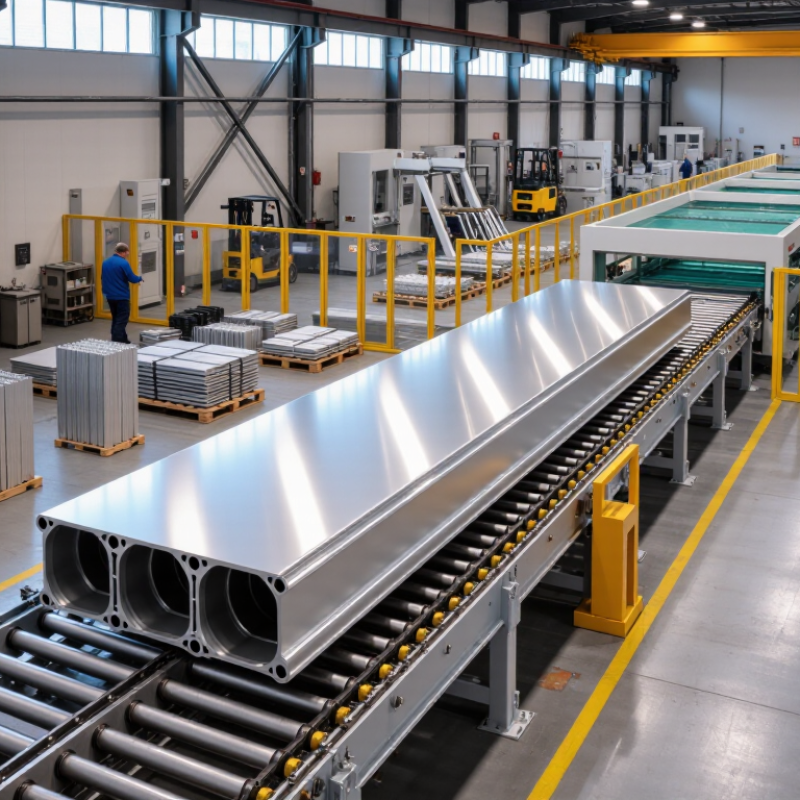
Aluminum Extrusion Basics for Global Buyers
Choosing an extrusion supplier starts with understanding the alloy, temper, press capacity, and achievable tolerances. These details affect cost, strength, appearance, and delivery reliability.
6063-T5 is widely used for frames, trims, and architectural profiles. It offers smooth surfaces and good corrosion resistance. However, it is not the strongest option. 6061-T6 provides higher strength for brackets, machine components, and structural parts. It is harder to extrude, especially with thin walls or complex shapes. Press tonnage must match the profile’s cross-sectional area, extrusion ratio, billet size, and required speed. A capable supplier should explain this calculation instead of quoting one fixed machine size.
Tolerances deserve practical attention. Standard limits may be acceptable for general profiles, but precision assemblies need drawing-based control. Ask for sample measurements, material certificates, and first-article inspection results. A perfect tolerance promise is a warning sign. Real production changes slightly with tooling wear, temperature, and straightening. I have found that early technical discussion prevents more problems than late price negotiation.
Tips: Keep wall thicknesses consistent. Avoid sudden thickness changes. Request a realistic tolerance review before tooling begins. Also, compare inspection methods, not only quoted prices. Surface quality can look excellent while dimensions quietly drift.
Supplier ranking should begin with evidence, not polished catalogs. The ISO Survey 2022 recorded more than 1.2 million ISO 9001 certificates worldwide. That scale shows broad adoption, not automatic quality. Buyers should verify certificate scope, expiration, issuing body, and actual production location. Ask for recent audit findings when possible. Small gaps matter.
EN 755 helps assess extruded profiles through mechanical properties and dimensional tolerances. ASTM B221 covers extruded aluminum bars, rods, wire, profiles, and tubes. A capable supplier should provide inspection records linked to these requirements. Compare alloy, temper, wall thickness, straightness, and surface condition. Do not accept “standard tolerance” without a clause reference. It sounds convenient, but it remains vague.
Traceability deserves equal weight. Each shipment should connect the billet or cast lot to press records, heat treatment, inspection results, and packing labels. The USGS Mineral Commodity Summaries 2024 estimated global primary aluminum production at about 70 million metric tons in 2023. Material volume is enormous. Documentation quality is uneven. During supplier reviews, request a sample material certificate and trace one serial number backward. This practical test reveals more than a presentation. A supplier may hold ISO 9001 certification yet lack clean lot-level records. That is an uncomfortable weakness, and ranking models should not hide it.
7 Best Aluminum Extrusion Parts Suppliers for Global Buyers
Seven Global Suppliers Compared by 600–15,000-Ton Press Capacity
Choosing an aluminum extrusion supplier starts with press capacity, not attractive catalogs. A 600-ton press suits small profiles, brackets, and thin decorative sections. A 1,500-ton machine handles medium rails, frames, and moderate wall thicknesses. For industrial beams, wide heat sinks, and large structural profiles, buyers may need 5,000 to 15,000 tons.
The seven supplier groups in this comparison cover this range. Suppliers with 600–1,500-ton presses often provide faster tooling changes and better flexibility for smaller batches. Mid-range facilities, using 2,000–5,000-ton presses, typically balance profile size, production volume, and tooling cost. The largest facilities can extrude broad sections, but their minimum order requirements may be less friendly to new projects.
Capacity changes everything. Yet press size alone proves little. Experienced buyers should request die drawings, alloy certificates, dimensional inspection reports, and sample cut sections. Check wall-thickness variation, surface marks, straightness, and aging consistency. A supplier may advertise 15,000 tons but lack suitable finishing or packaging controls.
I would also inspect practical details. Can the factory protect 6-meter profiles during ocean transport? Does it record billet temperature and quenching conditions? Are production records traceable by batch? My comparison is useful, but not perfect; machine lists can become outdated, and real output depends on tooling and operator skill. Ask for recent evidence. That gap matters.
| Supplier Profile | Primary Production Region | Press Capacity | Typical Billet Diameter | Approx. Maximum Profile Envelope | Common Alloy Coverage | Maximum Standard Cut Length | Surface Finishing Options | Quality & Compliance | Export Capability | Typical Production Lead Time | Best Fit for Global Buyers |
|---|---|---|---|---|---|---|---|---|---|---|---|
| Supplier A | East Asia | 600 tons | 3–5 inches | Up to approximately 120 mm | 6060, 6063, 6005A, 6061 | Up to 6,000 mm | Anodizing, powder coating, mill finish, precision cutting | ISO 9001; dimensional inspection; alloy and hardness testing | High-volume small-profile exports | 3–5 weeks after drawing approval | Lightweight trims, heat sinks, furniture sections, and small custom profiles |
| Supplier B | South Asia | 1,800 tons | 5–7 inches | Up to approximately 220 mm | 6063, 6061, 6005, 6082 | Up to 7,500 mm | Anodizing, electrophoretic coating, powder coating, wood-grain transfer | ISO 9001; ISO 14001; batch traceability | Strong container-load and mixed-order support | 4–6 weeks after tooling confirmation | Architectural frames, solar components, transport fittings, and general industrial parts |
| Supplier C | Central Europe | 3,000 tons | 7–9 inches | Up to approximately 320 mm | 6060, 6063, 6005A, 6061, 6082 | Up to 8,000 mm | Anodizing, powder coating, wet painting, machining, thermal break assembly | ISO 9001; ISO 14001; EN 755 and EN 12020 production controls | Reliable regional and cross-border delivery | 5–7 weeks after technical approval | Architectural systems, machine frames, precision enclosures, and engineered profiles |
| Supplier D | East Asia | 5,000 tons | 9–11 inches | Up to approximately 420 mm | 6063, 6061, 6005A, 6082, 7003 | Up to 12,000 mm | Anodizing, powder coating, fluorocarbon coating, brushing, CNC machining | ISO 9001; ISO 14001; production and final inspection records | Suitable for high-volume OEM programs | 5–8 weeks after die approval | Solar mounting systems, automotive structures, industrial frames, and long-length profiles |
| Supplier E | North America | 8,000 tons | 11–14 inches | Up to approximately 520 mm | 6061, 6063, 6005A, 6082, 6066 | Up to 14,000 mm | Mill finish, anodizing, powder coating, chemical conversion, fabrication | ISO 9001; IATF 16949 available for qualified automotive programs | Strong large-profile and domestic supply support | 6–10 weeks after design release | Automotive, heavy equipment, infrastructure, and large structural components |
| Supplier F | Western Europe | 10,000 tons | 14–16 inches | Up to approximately 650 mm | 6060, 6063, 6005A, 6061, 6082 | Up to 15,000 mm | Anodizing, powder coating, painting, CNC machining, assembly, thermal treatment | ISO 9001; ISO 14001; EN 755; controlled material certification | High compliance and multi-country logistics capability | 7–11 weeks after tooling and specification approval | Rail, renewable energy, premium architecture, and high-specification industrial parts |
| Supplier G | East Asia | 15,000 tons | 16–20 inches | Up to approximately 900 mm | 6061, 6063, 6005A, 6082, 7005, selected 7xxx alloys | Up to 16,000 mm | Mill finish, anodizing, powder coating, fluorocarbon coating, heavy fabrication | ISO 9001; ISO 14001; IATF 16949 available for approved programs | Best suited to very large profiles and long-term contracts | 8–14 weeks after engineering and die qualification | Large transport structures, energy infrastructure, industrial platforms, and oversized profiles |
Aluminum pricing often sets the first cost benchmark. The World Bank Commodity Markets Outlook reported average aluminum prices near US$2,400 per metric ton in 2024. Prices can change weekly with energy costs, inventories, and regional premiums. Ask suppliers to separate billet cost, conversion cost, and any metal surcharge. Otherwise, a low quotation may hide unstable pricing.
Die fees commonly range from US$500 to US$5,000 for standard profiles. Complex hollows, tight tolerances, and large dies can cost more. Small orders also create pressure. Many extruders set minimum order quantities between 300 and 1,000 kilograms. This figure varies by alloy, equipment, and production schedule. A practical buyer should request die ownership terms, trial-piece charges, and replacement costs. I have seen buyers focus on unit price, then discover that a small order makes the die uneconomical.
Finishing can add meaningful cost. Anodizing, powder coating, machining, and protective film require separate specifications. Freight is less predictable. UNCTAD’s Review of Maritime Transport 2024 described severe container-rate volatility during route disruptions. Ocean freight may therefore exceed the original quotation by a wide margin. Compare FOB, CIF, and delivered pricing on identical quantities. Include packing, inland transport, customs handling, and insurance. The cheapest supplier is not always cheaper after these details. That assumption deserves review.
Choosing among seven aluminum extrusion parts suppliers requires more than comparing unit prices. Global buyers should request a written lead-time schedule, including tooling, sampling, production, inspection, and ocean or air dispatch. A supplier promising ten days may exclude mold preparation. That gap matters.
Ask for physical samples made with the proposed alloy, surface finish, and tolerances. Measure wall thickness, hole position, straightness, and color consistency against your drawings. One sample is rarely enough. Request a small batch when appearance or assembly fit is critical. Keep inspection records, photographs, and signed specifications for later reference.
Certifications need careful checking. Confirm the certificate number, issuing body, scope, and validity date. Quality systems, material traceability, environmental controls, and product-specific test reports should match your project requirements. Do not accept a logo copied into a PDF. Verify it independently.
Export coverage also deserves practical questions. Can the supplier prepare commercial invoices, packing lists, certificates of origin, and export packaging? Ask which ports they regularly use and who handles freight claims. Check experience with your destination, not just a general “worldwide shipping” statement. A trial shipment can expose weak labeling, damaged corners, or unclear documentation before full production. Some buyers, including experienced teams, overlook this step when schedules become tight. That is an expensive lesson.
Ask for billet cost, conversion cost, and any metal surcharge. Include tooling, finishing, packing, inland transport, customs, and insurance. A low unit price may hide unstable metal pricing.
Standard dies commonly cost about US$500 to US$5,000. Complex hollows, tight tolerances, and large profiles may cost more. Ask about ownership, trial pieces, maintenance, and replacement costs. Small orders can make tooling uneconomical.
Many suppliers set minimum quantities between 300 and 1,000 kilograms. The actual amount depends on alloy, equipment, and production schedules. Request the minimum quantity in writing. Do not assume flexibility.
Anodizing, powder coating, machining, and protective film add separate costs. Specify color, thickness, gloss, masking, and surface protection. Appearance needs careful checking. Finish descriptions alone may be too vague.
Compare FOB, CIF, and delivered prices using identical quantities. Include packing, inland transport, customs handling, insurance, and possible freight claims. Container rates can change sharply during route disruptions. The cheapest quote may not remain cheapest.
Request separate dates for tooling, sampling, production, inspection, and dispatch. A promised ten-day lead time may exclude mold preparation. That difference can disrupt installation plans. Ask for a written schedule.
Samples reveal alloy, finish, wall thickness, hole position, straightness, and color consistency. Use the proposed production process. One sample is rarely enough for critical assembly parts. Keep measurements and photographs.
Confirm the certificate number, issuing body, scope, and validity date. Verify the document independently. A copied logo proves very little. Match traceability and test reports with project requirements.
Ask whether the supplier prepares invoices, packing lists, origin documents, and export packaging. Confirm regular ports and responsibility for freight claims. A trial shipment can reveal weak labels or damaged corners. This step is easy to skip.
This guide explains how global buyers can evaluate Aluminum Extrusion Parts suppliers with greater confidence. It covers essential technical fundamentals, including the differences between 6063-T5 and 6061-T6 alloys, press tonnage from 600 to 15,000 tons, and the role of dimensional tolerances in product performance. It also outlines practical supplier ranking criteria, such as ISO 9001 systems, EN 755 and ASTM B221 compliance, material traceability, production consistency, and export capability.
The comparison framework examines total purchasing cost, including aluminum pricing, custom die fees, minimum order quantities, surface finishing, packaging, and freight. Buyers will also find a due diligence checklist focused on realistic lead times, prototype samples, certification records, quality documentation, communication, and after-sales support. By reviewing these factors together, purchasing teams can identify reliable manufacturing partners, reduce unexpected costs, and select extrusion solutions that meet both technical requirements and international delivery expectations.
HG Precision